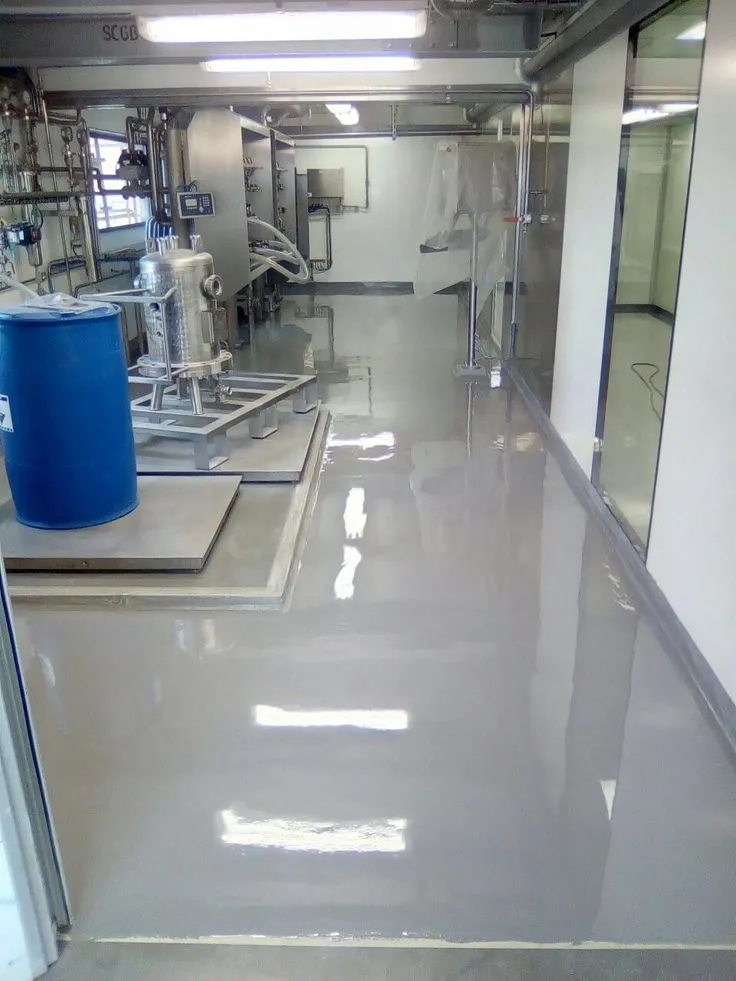
Boiler rooms place concrete floors beneath a mixture of heat, equipment weight, maintenance activity, water, and chemical-treatment processes. Pumps, tanks, valves, piping, and treatment equipment may occupy much of the available space, leaving narrow service routes for technicians. Small leaks or chemical drips can also occur repeatedly around the same locations. Because these conditions differ from ordinary storage or utility areas, boiler-room flooring should be planned around equipment servicing, water treatment, chemical exposure, and long-term access.
Water Treatment Creates Specific Exposure
Commercial boiler systems may use treatment products designed to manage scale, corrosion, or water quality. These chemicals are normally handled through controlled maintenance procedures, but the floor can still encounter occasional drips or spills.
Facility teams should document which products are stored or used in the room and how technicians handle them. Concentration, spill frequency, and cleanup procedures can all influence flooring requirements.
The phrase chemical resistance should therefore be connected to actual substances rather than treated as a generic feature.
Pumps and Valves Create Wet Zones
Boiler rooms contain numerous connections where water may appear during maintenance. Pump seals, valves, drain points, condensate systems, and piping work can all create localized moisture.
Facilities considering Epoxy Flooring For Mechanical Rooms should identify these wet-prone areas during the site assessment. The floor should remain practical to inspect and clean around equipment bases and utility connections.
A resinous system can help protect the concrete surface, but it cannot correct leaking equipment or major drainage problems.
Chemical Storage Needs Clear Organization
Treatment products should remain in designated storage locations according to facility procedures. Flooring can support organization through clearly defined zones where appropriate.
Managers may use floor markings to distinguish chemical-storage areas, service routes, or restricted equipment clearances. These visual boundaries should remain simple and should complement existing handling and safety procedures rather than replace them.
The floor around storage locations should also remain accessible for inspection and cleanup.
Heat Changes the Operating Environment
Boilers and associated piping can raise room temperatures, particularly in compact mechanical spaces. Some locations may also experience hotter surfaces or temperature changes during operation and shutdown.
The contractor should understand these conditions before recommending a flooring system. Resin selection should reflect the room’s realistic temperature environment as well as moisture, traffic, and chemical exposure.
Temperature is only one factor, but it should not be ignored simply because the concrete itself is not directly heated everywhere.
Concrete Preparation Is Critical
Older boiler rooms may contain multiple generations of paint, coatings, patches, oil staining, and chemical residue. Installing a new system over poorly prepared concrete can carry those weaknesses forward.
An Industrial Epoxy Flooring Contractor In Nj should explain how old coatings, weak concrete, cracks, and contamination will be addressed. Mechanical preparation can create a suitable profile while revealing damaged sections that require repair.
Tight areas around pumps, tanks, and curbs may need additional preparation beyond what large equipment can reach.
Drainage Should Be Evaluated Before Coating
Mechanical rooms often contain floor drains intended to handle maintenance water or minor leaks. The surrounding concrete should direct liquids toward those drains rather than allow them to collect beneath equipment.
Managers should observe where water moves during normal service and identify any low spots. Cracked drain surrounds, failed patches, or uneven transitions should be repaired before the new resinous floor is installed.
A coating should work with the room’s drainage design rather than be expected to correct significant slope deficiencies.
Texture Must Support Technicians
Boiler-room technicians may carry tools, move carts, or work close to water-treatment equipment. Practical traction can therefore be valuable in spill-prone locations.
However, excessive texture can make chemical or oil cleanup harder. The surface profile should balance footing with maintenance access and cleaning requirements.
Dry service corridors may not need the same texture as wet areas around pumps or chemical-treatment equipment.
Build Inspections Into Service Visits
Routine boiler maintenance provides a natural opportunity to inspect the floor. Technicians can watch for staining, chips, cracks, open edges, or changes near valves, tanks, drains, and equipment bases.
Recurring damage in one location may indicate a leak, vibration issue, chemical exposure, or substrate problem that deserves investigation.
Recording these patterns can help facility managers address the underlying cause instead of repeatedly repairing only the visible surface.
Conclusion
Boiler-room flooring needs to support an operating environment shaped by heat, water treatment, maintenance chemicals, pumps, drains, and restricted service access. These conditions make the space more demanding than a generic utility room.
A stronger flooring strategy begins with understanding how technicians actually service the equipment and where moisture or chemicals are most likely to reach the floor. Proper substrate preparation, suitable resin chemistry, effective drainage, practical texture, and routine inspection can create a more manageable surface while helping protect concrete around critical heating infrastructure.